Tap Drill Size Chart: UNC, UNF and Metric
The right drill for every common inch and metric tap, with decimal and mm sizes, the formula behind it, tap drills for NPT pipe threads, and clearance hole sizes for bolts that pass through.
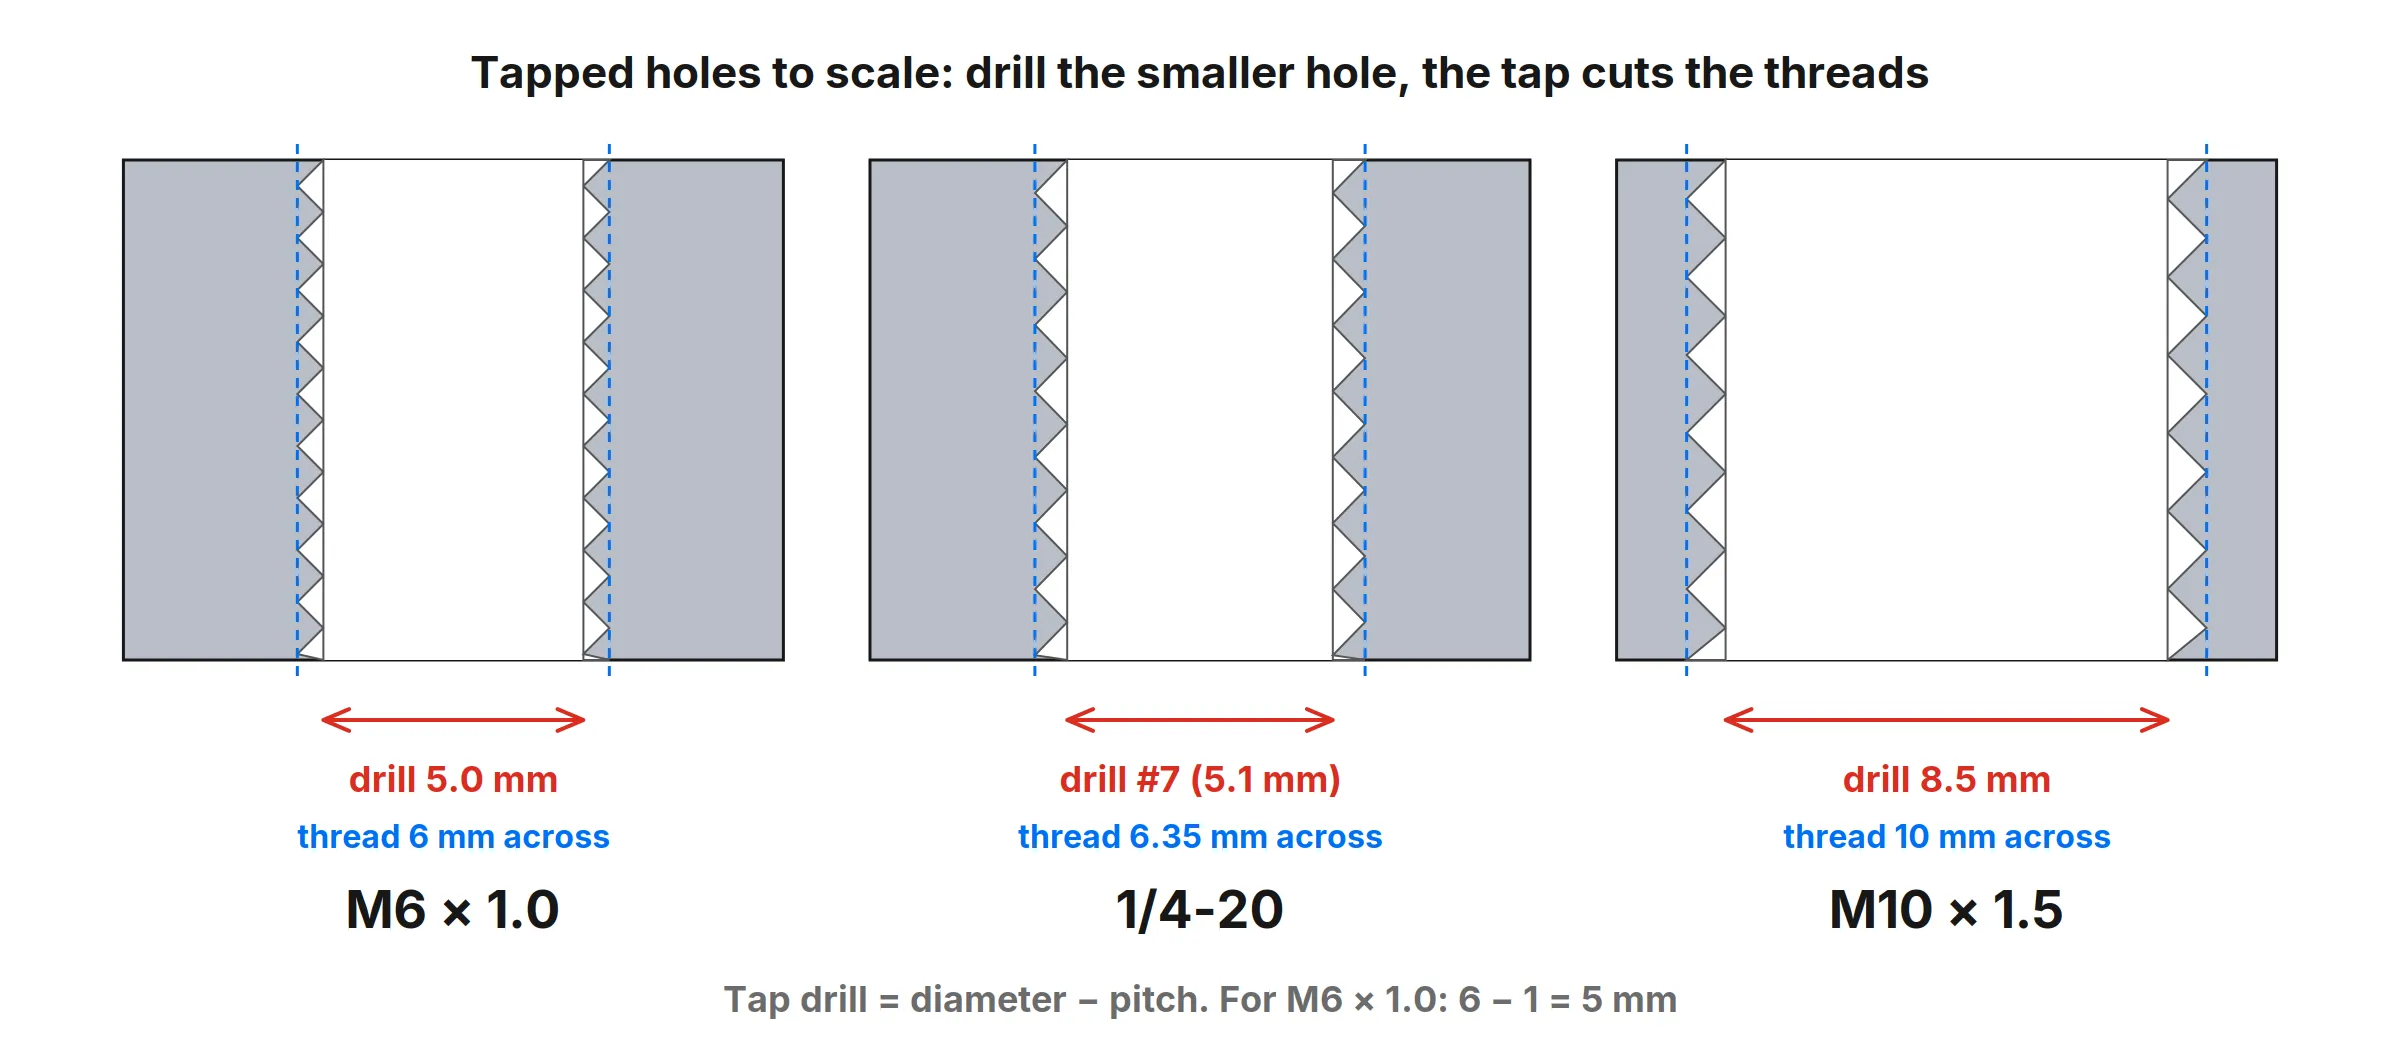
Before you cut threads with a tap, you drill a hole a little smaller than the bolt. The tap then cuts the threads into the material left around the hole. Drill too big and the threads are shallow and strip; drill too small and the tap binds and can snap. The sizes below give about 75% thread depth, the standard for most metal, plastic and hardwood.
Quick rule: tap drill = bolt diameter − pitch. For M6 × 1.0: 6 − 1 = 5 mm. Not sure which thread you have? Measure the bolt and use the thread identifier.
UNC and UNF tap drill chart
| Thread | Tap drill | Decimal (in) | mm |
|---|---|---|---|
| #0-80 | 3/64 | 0.0469 | 1.19 |
| #1-64 | #53 | 0.0595 | 1.51 |
| #2-56 | #50 | 0.0700 | 1.78 |
| #3-48 | #47 | 0.0785 | 1.99 |
| #4-40 | #43 | 0.0890 | 2.26 |
| #4-48 | #42 | 0.0935 | 2.37 |
| #5-40 | #38 | 0.1015 | 2.58 |
| #6-32 | #36 | 0.1065 | 2.71 |
| #6-40 | #33 | 0.1130 | 2.87 |
| #8-32 | #29 | 0.1360 | 3.45 |
| #8-36 | #29 | 0.1360 | 3.45 |
| #10-24 | #25 | 0.1495 | 3.80 |
| #10-32 | #21 | 0.1590 | 4.04 |
| #12-24 | #16 | 0.1770 | 4.50 |
| #12-28 | #14 | 0.1820 | 4.62 |
| 1/4-20 | #7 | 0.2010 | 5.11 |
| 1/4-28 | #3 | 0.2130 | 5.41 |
| 5/16-18 | F | 0.2570 | 6.53 |
| 5/16-24 | I | 0.2720 | 6.91 |
| 3/8-16 | 5/16 | 0.3125 | 7.94 |
| 3/8-24 | Q | 0.3320 | 8.43 |
| 7/16-14 | U | 0.3680 | 9.35 |
| 7/16-20 | 25/64 | 0.3906 | 9.92 |
| 1/2-13 | 27/64 | 0.4219 | 10.72 |
| 1/2-20 | 29/64 | 0.4531 | 11.51 |
| 9/16-12 | 31/64 | 0.4844 | 12.30 |
| 9/16-18 | 33/64 | 0.5156 | 13.10 |
| 5/8-11 | 17/32 | 0.5313 | 13.49 |
| 5/8-18 | 37/64 | 0.5781 | 14.68 |
| 3/4-10 | 21/32 | 0.6563 | 16.67 |
| 3/4-16 | 11/16 | 0.6875 | 17.46 |
| 7/8-9 | 49/64 | 0.7656 | 19.45 |
| 7/8-14 | 13/16 | 0.8125 | 20.64 |
| 1-8 | 7/8 | 0.8750 | 22.23 |
| 1-12 | 59/64 | 0.9219 | 23.42 |
The first number is the screw size and the second is threads per inch: 1/4-20 is a 1/4 inch screw with 20 threads per inch. In each pair, the lower number is UNC (coarse), the common hardware-store thread, and the higher is UNF (fine). Number and letter drills are listed with their sizes in the number and letter drill size chart.
Metric tap drill chart
| Thread | Pitch | Tap drill | Inch equivalent |
|---|---|---|---|
| M2 | 0.4 | 1.6 mm | #52 (0.0635) |
| M2.5 | 0.45 | 2.05 mm | #46 (0.081) |
| M3 | 0.5 | 2.5 mm | #40 (0.098) |
| M3.5 | 0.6 | 2.9 mm | #33 (0.113) |
| M4 | 0.7 | 3.3 mm | #30 (0.1285) |
| M5 | 0.8 | 4.2 mm | #19 (0.166) |
| M6 | 1.0 | 5.0 mm | #9 (0.196) |
| M8 | 1.25 | 6.8 mm | H (0.266) |
| M10 | 1.5 | 8.5 mm | Q (0.332) |
| M12 | 1.75 | 10.2 mm | Y (0.404) |
| M14 | 2.0 | 12.0 mm | 15/32 (0.469) |
| M16 | 2.0 | 14.0 mm | 35/64 (0.547) |
| M18 | 2.5 | 15.5 mm | 39/64 (0.609) |
| M20 | 2.5 | 17.5 mm | 11/16 (0.6875) |
| M24 | 3.0 | 21.0 mm | 53/64 (0.828) |
These are the standard coarse threads, the ones you get when no pitch is given. For fine metric threads, use the same rule:
| Fine thread | Tap drill |
|---|---|
| M8 × 1.0 | 7.0 mm |
| M10 × 1.25 | 8.8 mm |
| M10 × 1.0 | 9.0 mm |
| M12 × 1.5 | 10.5 mm |
| M12 × 1.25 | 10.8 mm |
| M14 × 1.5 | 12.5 mm |
| M16 × 1.5 | 14.5 mm |
| M20 × 1.5 | 18.5 mm |
Not sure of the pitch? See the thread pitch chart.
NPT pipe tap drill sizes
Pipe threads are tapered and sized by the pipe, not the hole, so the drill is much bigger than the name suggests.
| NPT size | Tap drill | Decimal (in) | mm |
|---|---|---|---|
| 1/8-27 | R | 0.339 | 8.6 |
| 1/4-18 | 7/16 | 0.4375 | 11.1 |
| 3/8-18 | 37/64 | 0.5781 | 14.7 |
| 1/2-14 | 23/32 | 0.7188 | 18.3 |
| 3/4-14 | 59/64 | 0.9219 | 23.4 |
| 1-11 1/2 | 1 5/32 | 1.1563 | 29.4 |
Tap until a fitting threads in by hand about 3 to 4 turns, then stop: the taper does the sealing. The pipe size chart explains why 1/2 inch pipe is 0.84 inch across.
Clearance holes
A clearance hole is the opposite of a tap drill: it goes in the part being bolted down, so the bolt slides through. A close fit locates parts accurately; a free fit is easier to line up.
| Bolt | Close fit | Free fit |
|---|---|---|
| #4 | #32 (0.116) | #30 (0.1285) |
| #6 | #27 (0.144) | #25 (0.1495) |
| #8 | #18 (0.1695) | #16 (0.177) |
| #10 | #9 (0.196) | #7 (0.201) |
| 1/4 | F (0.257) | H (0.266) |
| 5/16 | P (0.323) | Q (0.332) |
| 3/8 | W (0.386) | X (0.397) |
| 1/2 | 33/64 (0.516) | 17/32 (0.531) |
| Metric bolt | Close (fine) | Normal (medium) | Loose (coarse) |
|---|---|---|---|
| M3 | 3.2 mm | 3.4 mm | 3.6 mm |
| M4 | 4.3 mm | 4.5 mm | 4.8 mm |
| M5 | 5.3 mm | 5.5 mm | 5.8 mm |
| M6 | 6.4 mm | 6.6 mm | 7.0 mm |
| M8 | 8.4 mm | 9.0 mm | 10.0 mm |
| M10 | 10.5 mm | 11.0 mm | 12.0 mm |
| M12 | 13.0 mm | 13.5 mm | 14.5 mm |
| M16 | 17.0 mm | 17.5 mm | 18.5 mm |
Metric clearance holes are from ISO 273.
Tapping tips
- Drill straight. A drill press or a guide block keeps the hole square; a crooked hole makes a crooked thread.
- Use cutting oil on steel and aluminum (not on brass or cast iron, which tap best dry).
- Turn the tap a half turn forward, then a quarter turn back to break the chips, especially in blind holes.
- Soft or thin material? In aluminum, plastic or thin sheet, a drill one size smaller gives stronger threads. In hard steel, one size bigger makes tapping much easier with little loss of strength.
For drill bit sizes in fractions and mm, see the drill bit size chart; to convert any size, use inches to mm.
More DIY charts: number and letter drill sizes · bolt torque · washer sizes · screw and bolt sizes · thread pitch.
Frequently asked questions
What size drill for a 3/8-16 tap?
A 5/16 inch drill (0.3125 in, 7.94 mm). That leaves about 75% thread depth, the standard for steel and aluminum. For the fine thread 3/8-24, use a letter Q drill (0.332 in).
What size drill for a 1/4-20 tap?
A #7 drill (0.201 in, 5.11 mm). If you don't have number drills, 13/64 inch (0.203 in) is the nearest fractional bit and works in most materials. For 1/4-28, use a #3 drill (0.213 in).
How do you calculate the tap drill size?
Subtract the pitch from the diameter. For metric: M8 × 1.25 needs 8 − 1.25 = 6.75, rounded to a 6.8 mm drill. For inch threads, the pitch is 1 ÷ TPI: 1/2-13 needs 0.500 − 1/13 = 0.423 in, so a 27/64 drill (0.422 in).
What size drill for an M8 tap?
6.8 mm for the standard coarse M8 × 1.25 thread. For fine M8 × 1.0, use 7.0 mm. A 17/64 inch bit (6.75 mm) is the closest inch size if you don't have a 6.8 mm drill.
What size drill for a 1/8 NPT tap?
A letter R drill (0.339 in, 8.6 mm), or 11/32 inch (0.344 in) if you don't have letter drills. NPT pipe threads are tapered, so drill to depth and tap until a fitting threads in snugly by hand about 3 to 4 turns.
More measuring guides
- How to Read a Ruler (Inches and Centimeters)
- How to Read a Tape Measure
- How to Measure Without a Ruler
- Fraction to Decimal Inch Chart (with Millimeters)
- How to Measure Your Ring Size at Home
- Paper Sizes Chart (Inches and Millimeters)
- US Coin Sizes: Diameter, Thickness and Weight
- How to Use a Protractor
- How to Measure Your Height at Home
- How to Measure a TV or Monitor Screen Size
- How to Measure Your Foot for Shoe Size
- How to Measure Your Wrist for a Bracelet or Watch
- Picture Frame Sizes: Standard US and Metric Chart
- Lumber Sizes: Actual vs Nominal Dimensions Chart
- Mattress and Bed Size Chart: US Dimensions in Inches and cm
- Ring Size Chart: US, UK, EU and Japan Conversion
- Necklace Length Chart: How Each Chain Length Fits
- Free Printable Ruler Worksheets with Answer Keys
- Screw and Bolt Size Chart: US and Metric
- Drill Bit Size Chart: Inch, Metric and Tap Drill Sizes
- Nail Size Chart: Penny Sizes Explained
- Envelope Sizes Chart: US and International
- Business Card Size: Standard Dimensions by Country
- Poster Sizes Chart: US and International
- Hat Size Chart: How to Find Your Hat Size
- Pandora Ring Size Chart: Pandora to US and UK Sizes
- Cartier Ring Size Chart: Cartier to US and UK Sizes
- How to Measure for Curtains in 5 Steps
- How High to Hang Curtains (and Why Higher Looks Better)
- Curtain Size Chart: Standard Lengths and Widths
- Wrench Size Chart: SAE vs Metric, Sockets and Allen Keys
- Wire Gauge Chart: AWG Sizes in Inches and mm
- Pipe Size Chart: Nominal vs Actual Sizes
- Sandpaper Grit Chart: Which Grit for Which Job
- Thread Pitch Chart: UNC, UNF and Metric Threads
- Sheet Metal Gauge Chart: Thickness in Inches and mm
- Extension Cord Gauge Chart: Length, Amps and AWG
- Rebar Size Chart: US Bar Sizes, Diameter and Weight
- Plywood and Drywall Thickness: Nominal vs Actual
- Number and Letter Drill Size Chart
- Bolt Torque Chart: SAE Grades and Metric Classes
- Washer Size Chart: SAE, USS and Metric Washers
- How to Show the Ruler in Word
- How to Show the Ruler in Google Docs
- How to Show the Ruler in PowerPoint
- Is an Online Ruler Accurate? How to Calibrate It
- How to Measure Inches on Your Phone
- How Big Is 1 Inch? Everyday Objects That Are an Inch
- How Big Is 1 cm and 1 mm? Real-Life Comparisons
- How to Measure PD (Pupillary Distance) for Glasses
- Ear Gauge Size Chart: Gauge to mm and Inches
- Bra Size Chart and How to Measure for a Bra